Clean the screw without machine teardown
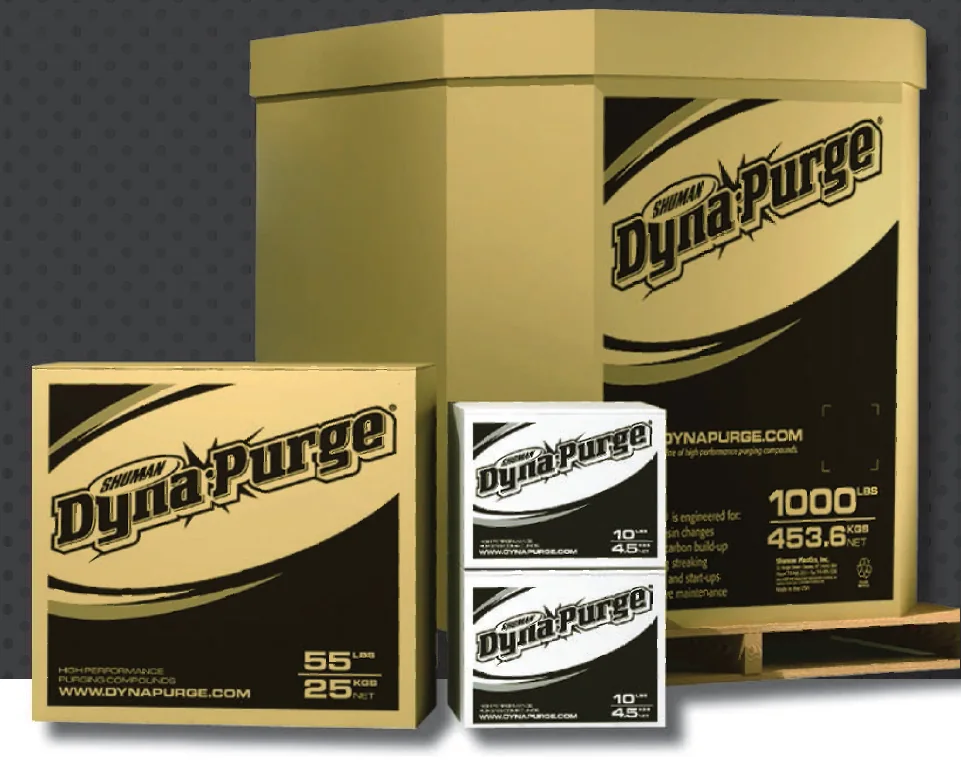
Dyna-Purge D2 is an engineered grade using Shuman Plastics’ exclusive “3X” technology. It acts on the process boundary layers as well as negative-flow and stagnation points, where old resin and color tend to hang up. D2 softens without flowing, loosens degraded material and pushes it out of the system without wearing the screw.
Primary applications
- Color changes and resin changes
- Preventive machine maintenance
- Before manual cleaning
- Shutdown and start-up
Equipment and processes
D2 is used for injection molding with hot and cold runners, and for extrusion of profile, sheet, blown film and cast film, compounding and blow molding. The Product Information Sheet lists D2 for all resin types within its operating temperature range.
Key operating data
* Actual quantity depends on machine condition and contamination level.
Features
- Easy to use: no process adjustment, mixing or soaking required.
- Safe, non-hazardous ingredients; FDA compliant.
- Heat stable; recommended during shutdown and start-up.
- Low cost-per-purge: a small quantity is effective.
- Recyclable.
- Unlimited shelf life.
Barrel and screw cleaning procedure
- Maintain the current resin’s speed and temperature.
- Retract the nozzle from the mold to allow purging.
- Clean the feed hopper completely.
- Run out the current resin.
- Add Dyna-Purge D2 into the hopper or hopper throat, one scoop at a time.
- The purge exits through the die, nozzle or accumulator.
- Continue adding D2 until the machine is clean.
- Adjust temperature for the new resin.
- Feed the new resin to push out the remaining D2.
- Start production with the new resin.
Frequently asked questions
Which resins can D2 be used with?
All resins processed between 160 and 329°C.
How much D2 is needed per purge?
About 1–2 times barrel capacity. The actual amount depends on how contaminated the machine is. Send your barrel capacity and GKFRP will estimate the quantity.
Do I need to change temperature or screw speed to purge?
No. Keep the current resin’s conditions; adjust temperature only after purging, before feeding the new resin.
Can D2 be used with hot runner molds?
Yes. D2 is used for both hot and cold runners.
Can D2 be used before a long shutdown?
Yes. D2 is heat stable and recommended before shutdown and at start-up.
What is the shelf life?
Unlimited.
Actual purge quantity depends on screw/barrel design, hot runner or die configuration, previous and next resin, carbon build-up and machine condition.