Prepare a compatible material system
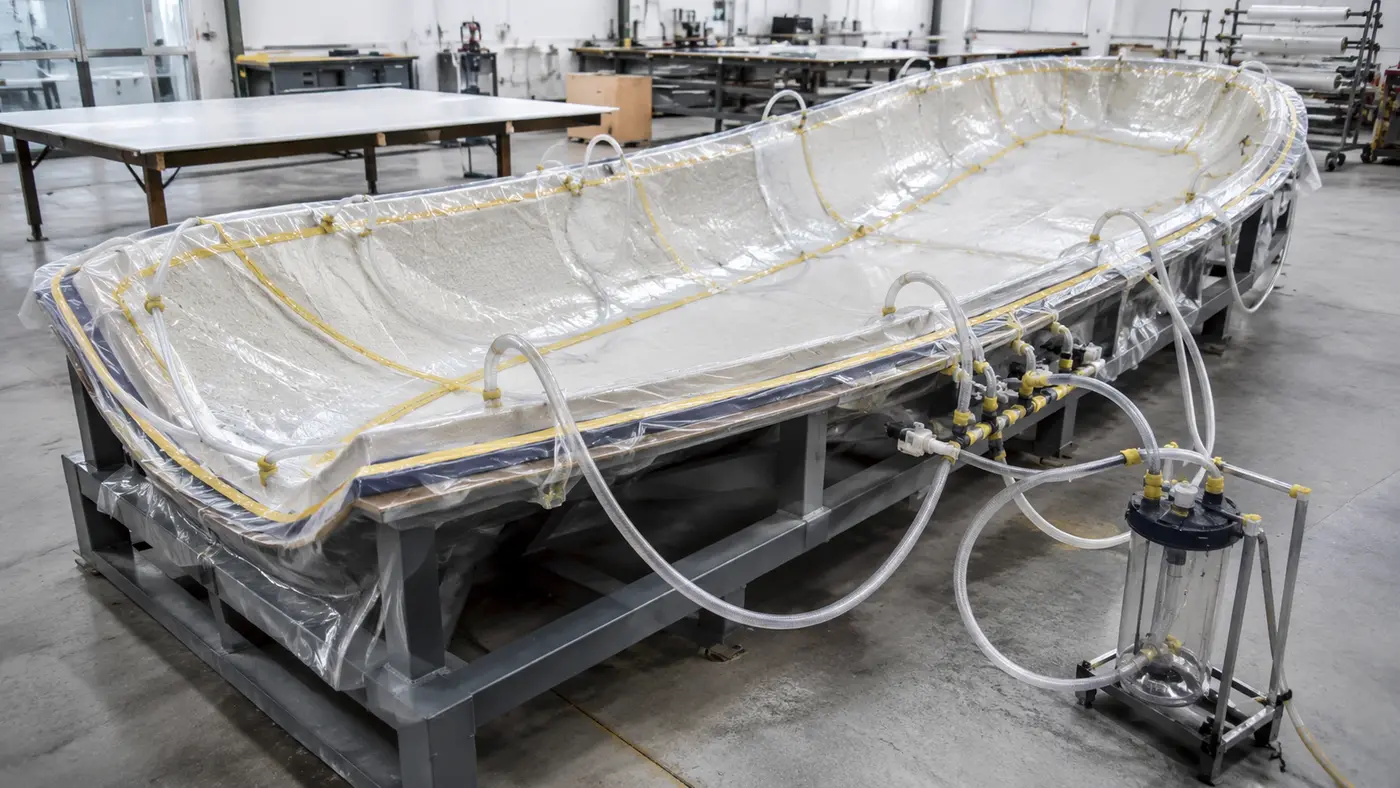
Infusion resin, reinforcement, peel ply, flow media, vacuum bag and resin lines must suit part size and fill time.
Verify vacuum integrity before infusion
Stable vacuum and a leak test reduce air entrapment, dry spots and resin-content variation.
Control resin flow
Feed and vacuum locations, flow-media selection and resin viscosity determine the flow front and infusion time.
Typical layer stack
From the mold surface outward: mold release, gelcoat (if used), dry reinforcement and core, peel ply, infusion mesh, spiral tube for resin feed and vacuum line, and vacuum bagging film sealed with sealant tape.
Choosing an infusion resin
An infusion resin needs low viscosity to fill the laminate before gel, a gel time long enough for the part size, and controlled exotherm in thick laminates. Polyester, vinyl ester and epoxy all have infusion grades; choose by mechanical requirements, service environment and cost.
Common defects
- Dry areas: blocked flow paths, mesh ending too early or resin gelling before fill.
- Voids: leaks, dissolved air in the resin or aggressive mixing.
- Resin-rich laminate: low compaction or an unsuitable consumable stack.
- Bridging at corners: no pleats left in the bag film.